Independent machinery sourcing · Integration

CNC machining center

Cnc Machining Center Sourcing coordinates factory quotes for a CNC machining center when the buyer can describe the workpiece, fixture concept, quantity and destination. Public machine data sheets separate axis travel, table size, table load, spindle speed and tool-changer limits; those columns are comparison units, not a promise that your fixture and longest tool will clear the spindle-to-table envelope.

This site is an independent sourcing partner. We do not manufacture machining centers, keep inventory, or sign factory acceptance. Read the envelope checklist before treating linear travel as usable workspace. Manual mills belong on a different inquiry family.

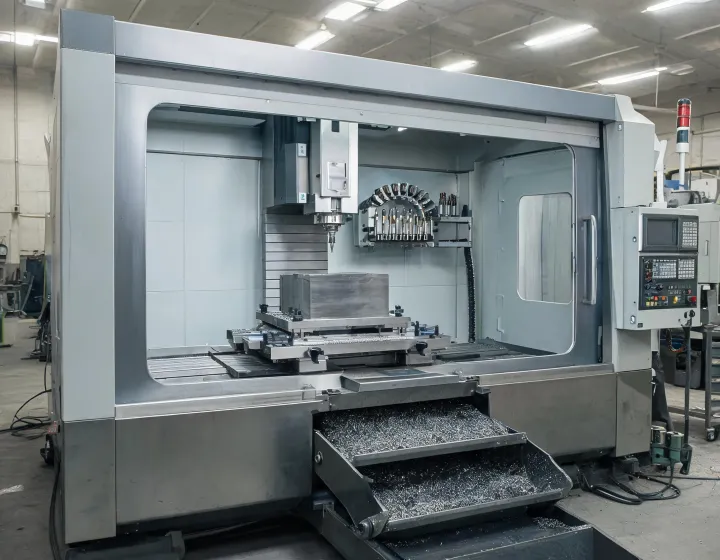
Request Factory Quotes Vertical CNC machining center cutting a fixtured steel workpiece in a metalworking shop

Site interface register

Connections to confirm
Interface Buyer input
Electrical Voltage, phase and frequency for the spindle drive and cabinet; connected load in kW after the supplier sizes the installation, not a guessed shop average.
Utilities Compressed air for tool unclamp or pallet clamps if used; coolant type; chip conveyor pit or scraper path; extraction if mist collection is quoted.
Controls Control brand preference if any, probing macros, postprocessor handoff, and which PLC or cell signals must handshake with a robot or pallet pool.

Included and separately quoted

A CNC machining center RFQ is comparable only after each bidder uses the same split between the base machine, first fixture and tool package, and work that stays on the plant side. Spindle rpm and rapid rates are not acceptance criteria unless the material, tool list and inspection method sit next to them.

Base machine

  • Machine structure, spindle, axis travels as published, guarding and chip handling as a standalone cell, without assuming a robot cell is in the same price.
  • Standard tool magazine and probing kit only if the quote names pocket count, max tool diameter and max tool weight.

Replacement versus a new CNC machining center bay

Existing process

Many shops swap a worn vertical mill while keeping the same vise, rotary table and longest tool. That only works if the new spindle-to-table envelope still clears that stack, and if table load includes the fixture mass rather than the blank alone.

Write whether the incoming machine must sit on the current grout pattern and chip pit, or whether a greenfield pad is acceptable, before ranking two vertical envelopes.

Documents that change a CNC machining center quote

Does the fixture and tool stack fit the spindle-to-table envelope?
  • Drawing or process description

    Send workpiece size, fixture height, longest tool, and any rotary or trunnion. Ask the supplier to check collisions through the programmed travel, not only X/Y/Z nameplate numbers. Haas VF-2 literature is a public example of how travel, table load and tool-changer limits are listed separately; using those categories is a comparison method, not an affiliation.

  • Operating conditions

    Name material, coolant, chip load and whether probing is in-cycle. Mass on the table should count the fixture and any rotary table, not only the blank. Magazine diameter or weight limits belong next to the heavy tools, not as a later surprise.

Missing fixture height or tool length is not filled with a typical shop value. Mark the unknown so bidders quote the same gap instead of inventing clearance.

Which procurement scope is covered, and who keeps which responsibilities?

Scope is CNC machining center procurement for US plant buyers. Cnc Machining Center Sourcing matches factories and compares wholesale quotations. Engineering acceptance, installation quality and process validation remain in the contract between buyer and equipment supplier. See cycle-estimate notes and the equipment options.

Request factory quotes for a CNC machining center

Discuss Your Requirements